Skip To Content

Products

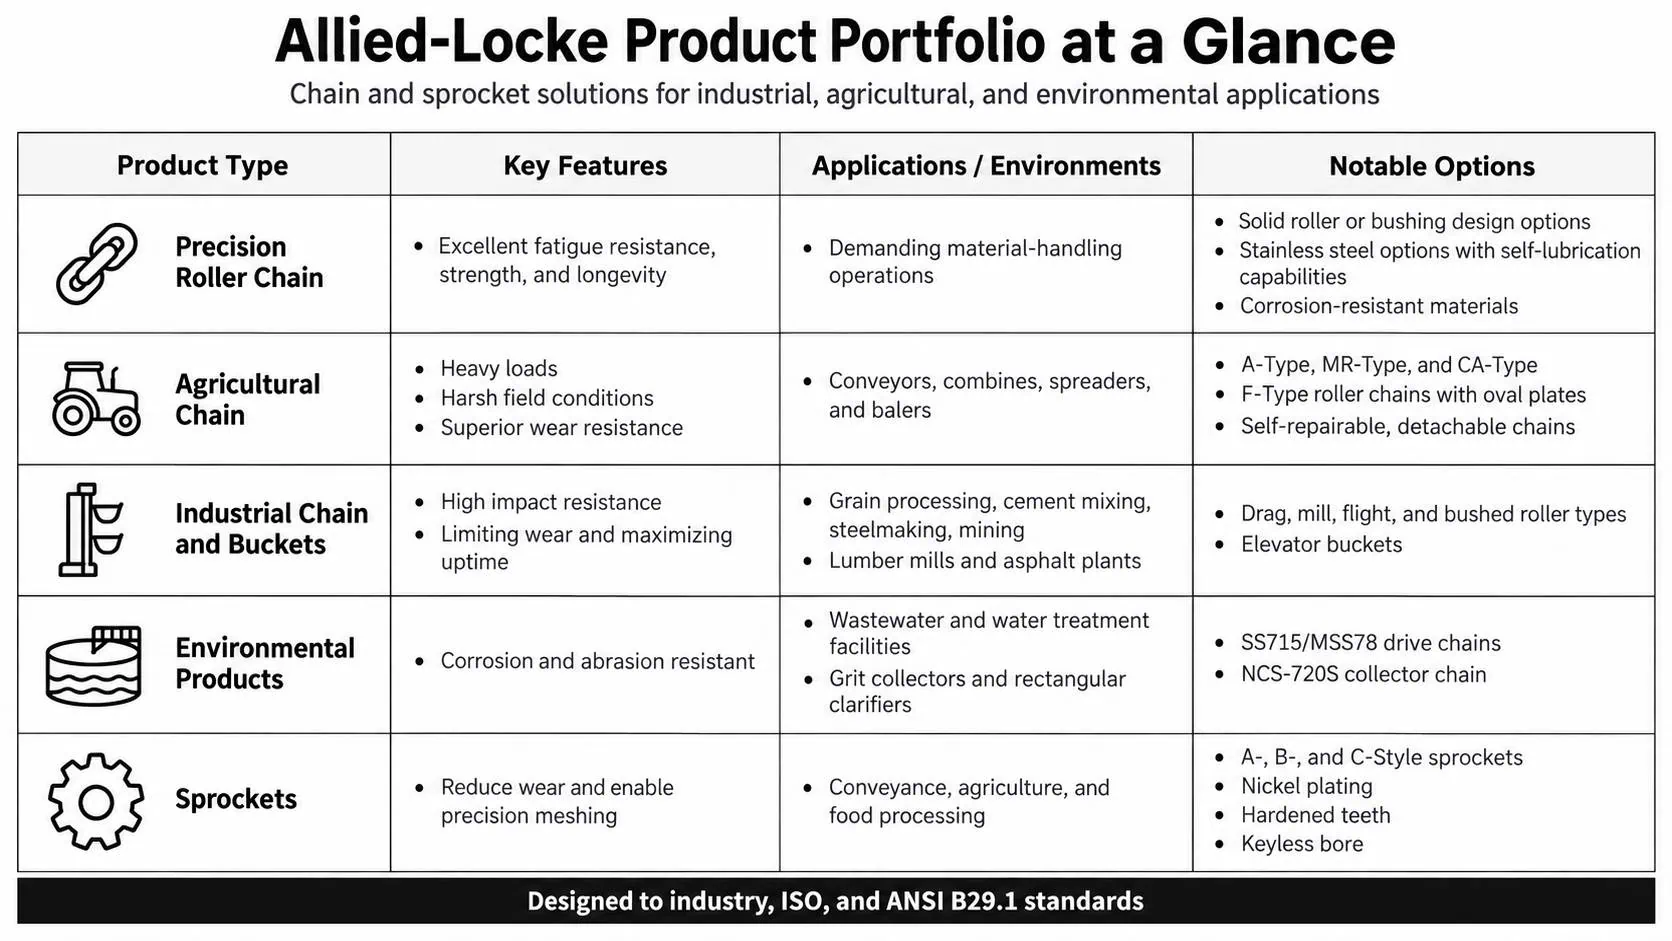
Allied-Locke Industries is a leading chain and sprocket manufacturer, providing high-quality solutions for the agricultural, industrial, and environmental industries. Our industrial roller chains and other products offer superior performance for municipal systems, OEMs, and maintenance teams in need of reliable chains and sprockets for conveyance, lifting, and material transport applications. All of our products are designed to industry, ISO, and ANSI B29.1 standards to optimize performance and service life.

Find out more about our products, their features, and some common applications.
Precision Roller Chain

Our roller chain products have excellent fatigue resistance, strength, and longevity for reliable use in demanding environments. Key roller chain features include:

They are interchangeable, with advanced attachment design and hardened elements, making them suitable for heavy use.

They are interchangeable, with advanced attachment design and hardened elements, making them suitable for heavy use. These chains can also support demanding material-handling operations that require durable components, including applications that connect with steel mill chains and other heavy-duty conveyor systems. 

  • Solid roller or bushing design options.
  • Advanced attachment design and hardened elements.
  • Compliance with ISO and ANSI standards for interchangeability and quality.
  • Stainless steel options with self-lubrication capabilities.
  • Corrosion-resistant materials.
  • Resilient, high-load hooked cotter or super chains with high shear strength.

View Our Catalog

Agricultural Chain

At Allied-Locke, our agricultural chains handle heavy loads and withstand harsh field conditions. Multiple formats are available with different tensile strengths, including A-Type, MR-Type, and CA-Type chains for use in conveyors, combines, spreaders, and balers. A variety of compatible attachments is also available, such as pushers, slats, and flights.

We manufacture our agricultural chains for superior wear resistance and reduced maintenance requirements, which is beneficial in high-cycle, dusty, or muddy environments. F-Type roller chains with oval plates offer greater durability and increased clearance in these applications. Self-repairable, detachable chains are also available for applications that need efficient field servicing for minimal downtime.

These durable chain options are suited to a variety of conveying environments, complementing specialized products such as lumber mill conveyor chains, where reliable material movement is required.

View Our Catalog

Industrial Chain and Buckets

Allied-Locke offers heavy-duty industrial chain and bucket solutions for many bulk materials in grain processing, cement mixing, steelmaking, mining, and other applications. Our steel mill chains and cement conveyor chains are built for demanding material-handling environments, while our solutions also serve lumber mills and asphalt plants. Chain products come in drag, mill, flight, and bushed roller types, among others, and they are available with elevator buckets suitable for use with high temperatures, abrasives, or other industrial conditions. These heavy-duty chain systems optimize efficiency with high impact resistance, while limiting wear and maximizing uptime.

Allied-Locke also provides solutions for customers looking for asphalt plant conveyor chain suppliers, with chain products suited to demanding conveying and material transport applications. Our industrial chain products can also support applications requiring lumber mill conveyor chains, where chains must withstand repeated use and challenging operating conditions.

To increase service life and abrasion resistance, our buckets incorporate induction-hardened pins and through-hardened sideplates. To bolster our elevator buckets, we use Renold-style chains that withstand shock loading for increased durability. These buckets also support continuous operation with forged central chains, allowing for the efficient handling of grain, clinker, ore, and sand.

For operations handling abrasive or heavy materials, cement conveyor chains and steel mill chains can provide the durability needed for continuous industrial conveying. These applications benefit from chain systems built to handle demanding loads, impact, and wear.

Elevator buckets are also durable in high temperatures and resist wear and damage from abrasives during cleanup and resets, and they enable a secure connection to belts and chains.

View Our Catalog

Environmental Products

Our collector and driver chains are designed for use in wastewater and water treatment facilities, with applications for grit collectors and rectangular clarifiers. Corrosion and abrasion resistant stainless steel SS715/MSS78 drive chains are available, as well as non-metallic NCS-720S collector chain in clarifier environments.

These systems also prevent potential grit accumulation and rotation using our unique pin design and glass-reinforced nylon links, both of which increase lifespan and durability for use in many plants.

The company’s broad range of industrial chain products also makes Allied-Locke a resource for demanding plant environments, including operations that require asphalt plant conveyor chain suppliers with experience in heavy-duty conveying applications.

View Our Catalog

Sprockets

Our sprocket products are compatible with all chain types and help reduce wear and enable precision meshing. Depending on your needs, we offer A-, B-, and C-Style sprockets that are available in stainless steel and carbon steel or cast materials, all within ANSI compliance. Other features include fully customized keyless and keyless bore, nickel plating, and hardened teeth for use in conveyance, agriculture, and food processing applications.

Sprockets can complement a wide range of chain systems, including heavy-duty products used alongside steel mill chains, cement conveyor chains, and other industrial conveying solutions.

View Our Catalog

Find the Right Chain and Sprocket Solution Today

Allied-Locke is the smart, reliable choice for industrial roller chains, elevator buckets, sprockets, and related equipment. With a wide range of options for different industries and applications, we can direct you to the right chain and industrial sprocket solutions for improved efficiency with minimal maintenance. Our products can significantly increase uptime and cost-effectiveness for nearly any industrial application.

Whether you need lumber mill conveyor chains, cement conveyor chains, steel mill chains, or other industrial chain products, Allied-Locke offers solutions for demanding material-handling applications.

Request a quote for your application today!

Frequently Asked Questions

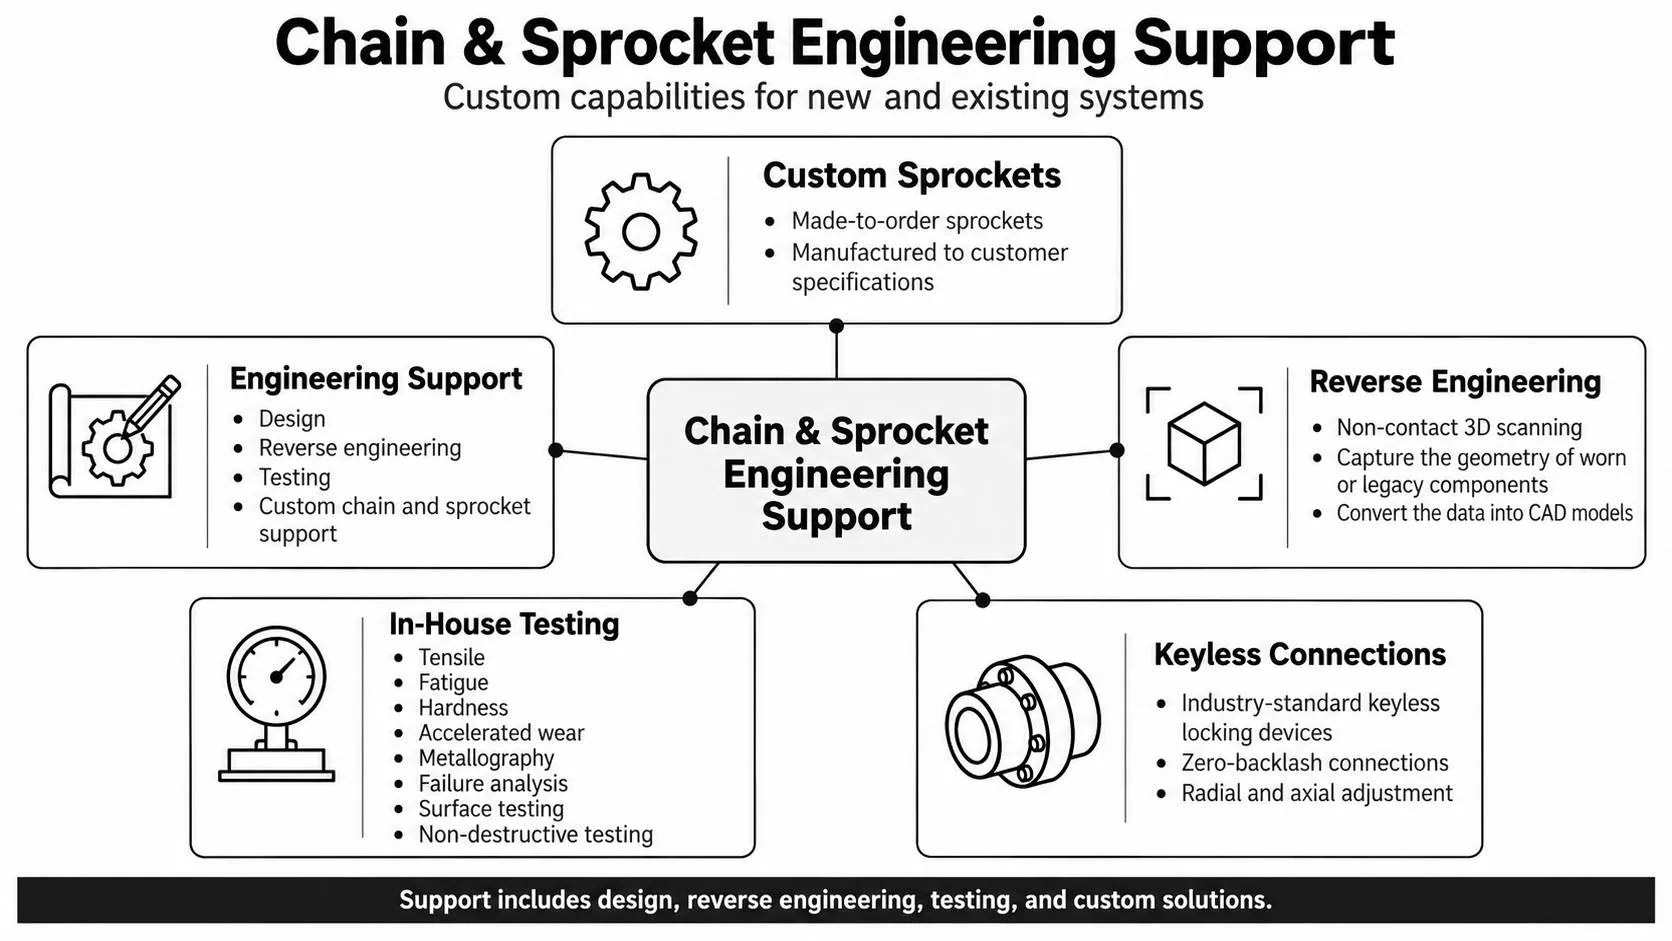
Yes. Allied-Locke offers made-to-order sprockets for non-standard requirements and can manufacture them to customer specifications.

Yes. Its in-house engineering team provides design, reverse engineering, testing, and custom chain and sprocket support for new and existing systems.

Yes. Allied-Locke uses non-contact 3D scanning to capture the geometry of worn or legacy components and convert the data into CAD models for replication or design updates.

Its in-house capabilities include tensile, fatigue, hardness, accelerated wear, metallography, failure analysis, surface testing, and non-destructive testing.

Yes. Allied-Locke offers sprockets bored for industry-standard keyless locking devices, which can provide zero-backlash connections and allow radial and axial adjustment.

Request a quote or View our product catalog

Request a quote