

Asphalt & Cement Plant Chains
Asphalt and cement plants depend on chain-driven equipment to move heavy, abrasive materials through demanding production environments. Allied-Locke Industries manufactures industrial chains and related components for these applications, with products built for conveying, elevating, and material handling.
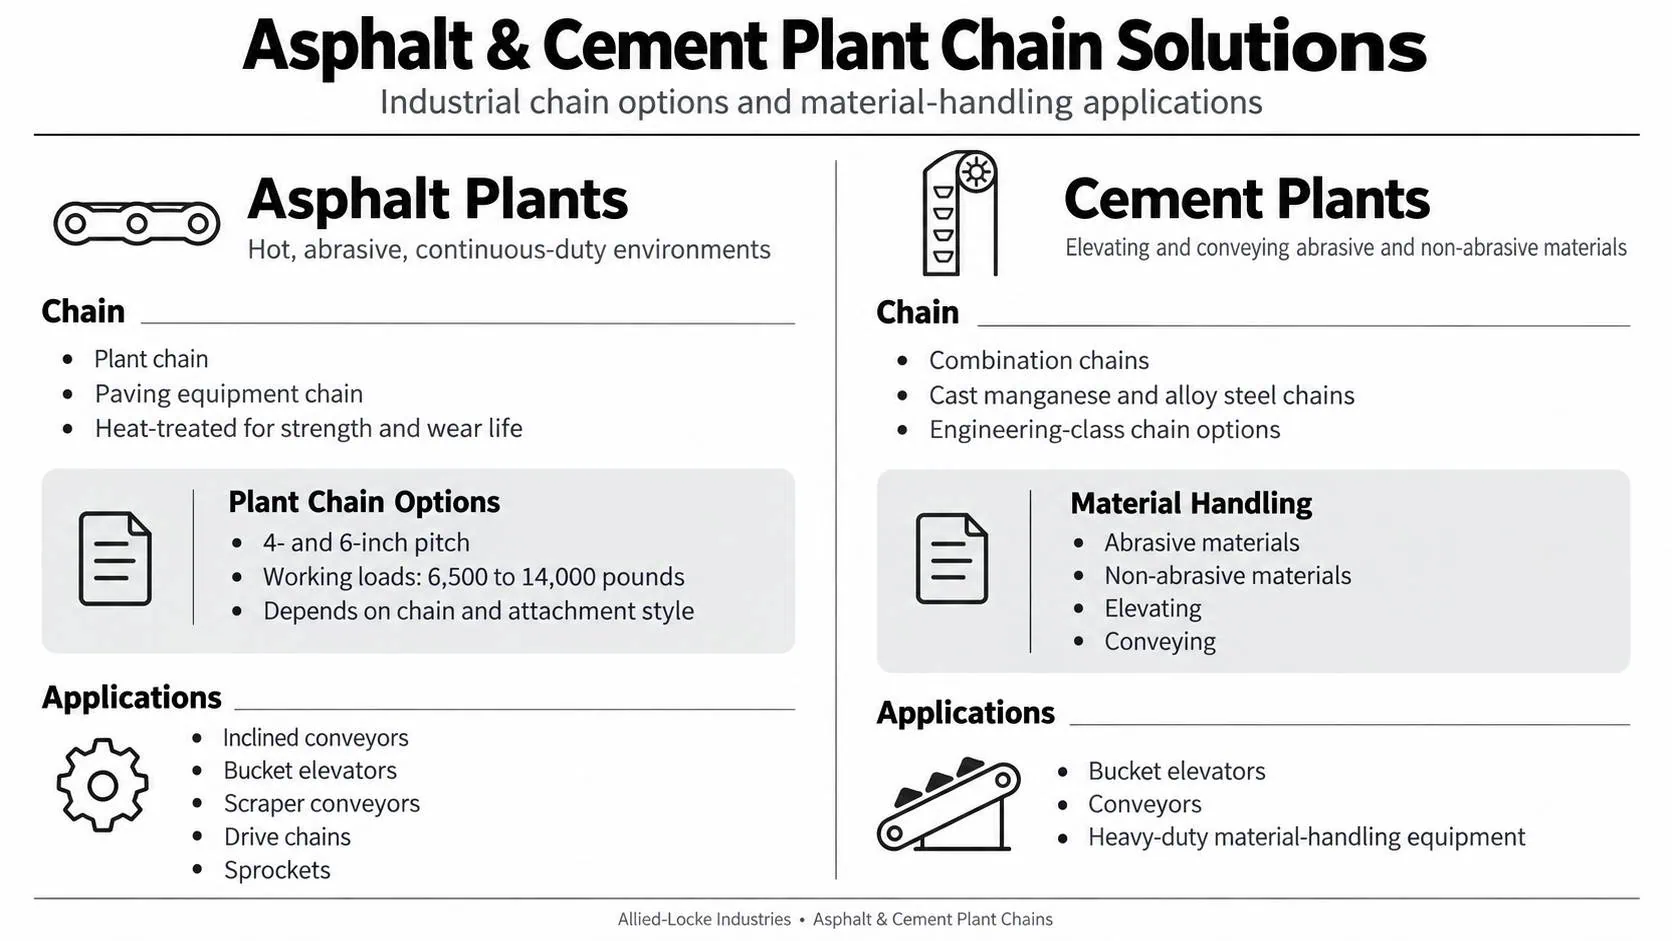
For asphalt operations, Allied-Locke supplies plant chain and paving equipment chains. Its asphalt chains are heat-treated for strength and wear life in hot, abrasive, continuous-duty environments. Available plant chain configurations include 4- and 6-inch pitch options with working loads ranging from 6,500 to 14,000 pounds, depending on the chain and attachment style.
As one of the established asphalt plant conveyor chain suppliers in the USA, Allied-Locke supports applications such as inclined conveyors, bucket elevators, scraper conveyors, drive chains, and sprockets.
For cement facilities, cement conveyor chains provide the strength and configuration needed for elevating and conveying abrasive and non-abrasive materials. Allied-Locke offers combination chains, cast manganese and alloy steel chains, and other engineering-class chain options for demanding material-handling systems. Its combination chains are available in multiple pitches and working-load capacities.
Asphalt and Cement Plant Buckets & Conveyor Systems
The chain is only one part of a complete material-handling system. Allied-Locke also offers components used with bucket elevators and conveyor equipment for cement plant applications.
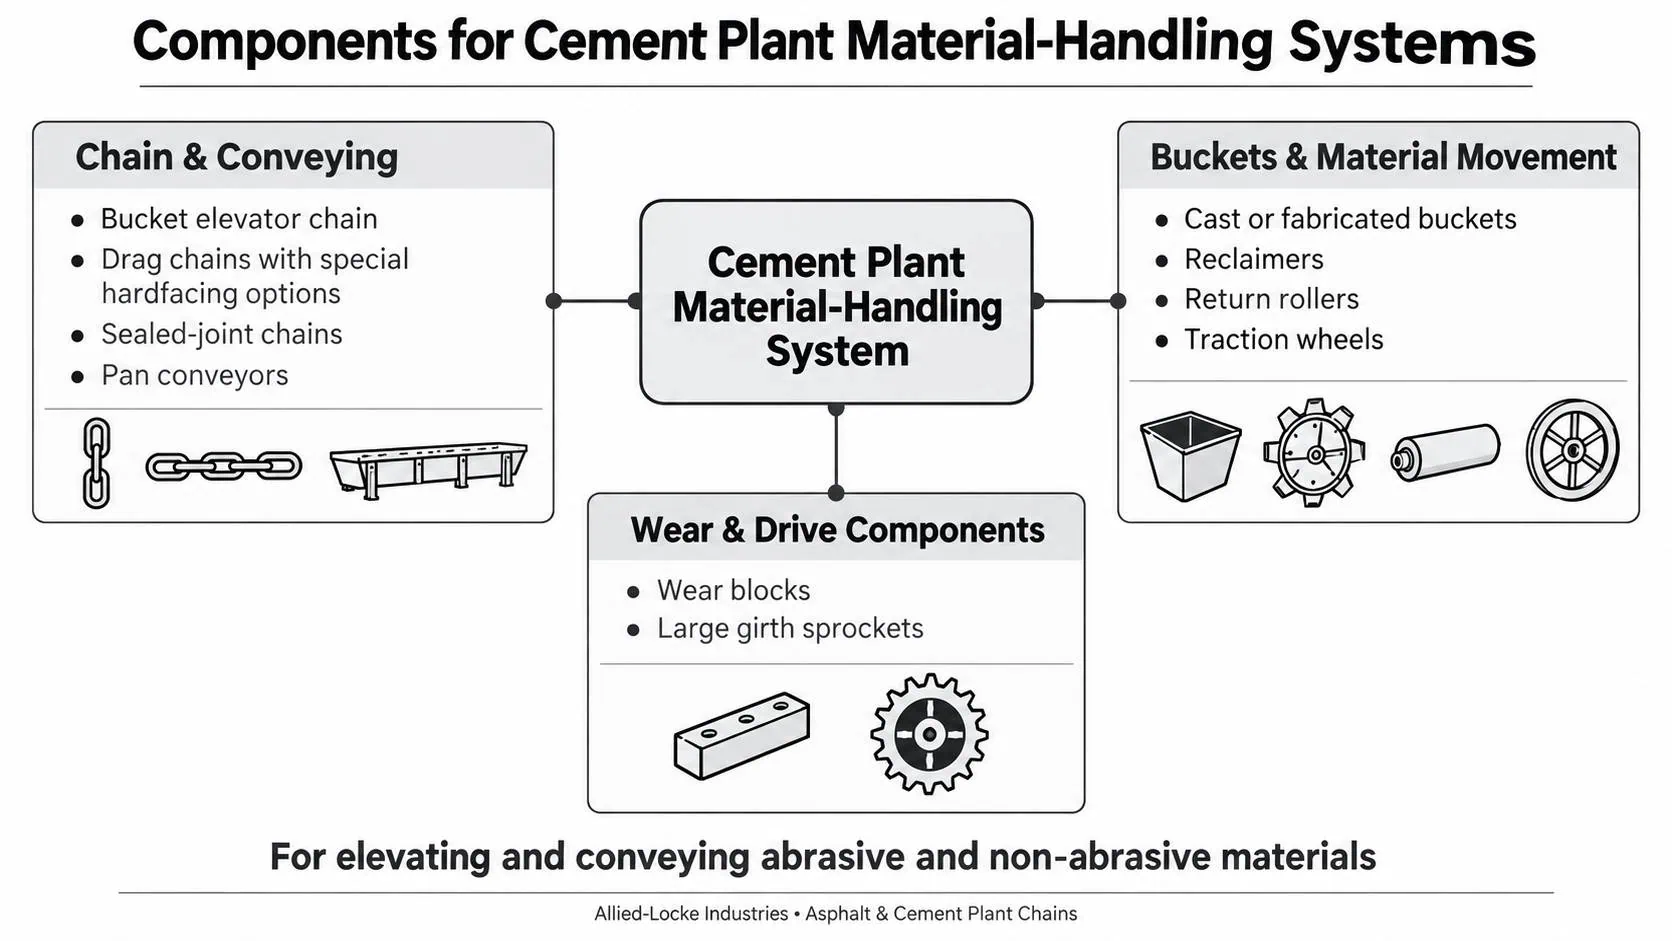
Its cement plant product range includes:
- Bucket elevator chain
- Cast or fabricated buckets
- Reclaimers
- Drag chains with special hardfacing options
- Wear blocks
- Pan conveyors
- Sealed-joint chains
- Large girth sprockets
- Return rollers
- Traction wheels
These components can support systems used to move bulk materials throughout a cement plant. Allied-Locke’s combination chains are also used extensively for elevating and conveying abrasive and non-abrasive materials.
For asphalt facilities, Allied-Locke’s product information identifies inclined conveyors, bucket elevators, scraper conveyors, drive chains, and sprockets among the applications served. This range allows customers to source chain and associated components for different points within their material-handling equipment.
Catalog
Allied-Locke offers a broad selection of engineering-class chains and buckets that can be specified according to equipment requirements. Relevant product families include combination chains, cast manganese and alloy steel chains, SS Class bushed steel chains, MSR Class bushed roller steel chains, welded steel chains, and elevator buckets.
The final product listings for this page should be confirmed with Allied-Locke to identify the specific asphalt and cement plant chains, buckets, attachments, and conveyor components currently available. Product specifications can include pitch, working load, dimensions, attachment style, and construction.
Quality Assurance
Allied-Locke has manufactured chains and sprockets for the asphalt industry since 1965 and identifies its products as manufactured in the USA. Its asphalt plant chains are heat-treated to support strength and wear life, while its industrial product range includes chains manufactured for demanding conveying and elevating applications.
Allied-Locke operates its primary manufacturing facility in Dixon, Illinois, which covers nearly 675,000 square feet. Allied-Locke is also ISO certified and emphasizes quality control throughout its manufacturing operations.
Work With Us
Whether you need asphalt plant conveyor chain suppliers for a new conveying system or reliable cement conveyor chains for an existing plant, Allied-Locke can help identify chain and component options for your application. Contact Allied-Locke Industries to discuss your requirements, request product information, or obtain a quote.